PC/PS 소재의 성형 온도를 최적화하는 방법
Forming temperature is the single most influential variable in carrier tape manufacturing. It determines whether the heated polymer flows uniformly into the mold cavity, whether pocket walls maintain consistent thickness, and whether the finished tape holds dimensional tolerance after cooling. For polycarbonate (PC) and polystyrene (PS)—the two dominant materials in precision carrier tape production—the processing windows differ significantly, and each requires distinct temperature control strategies.
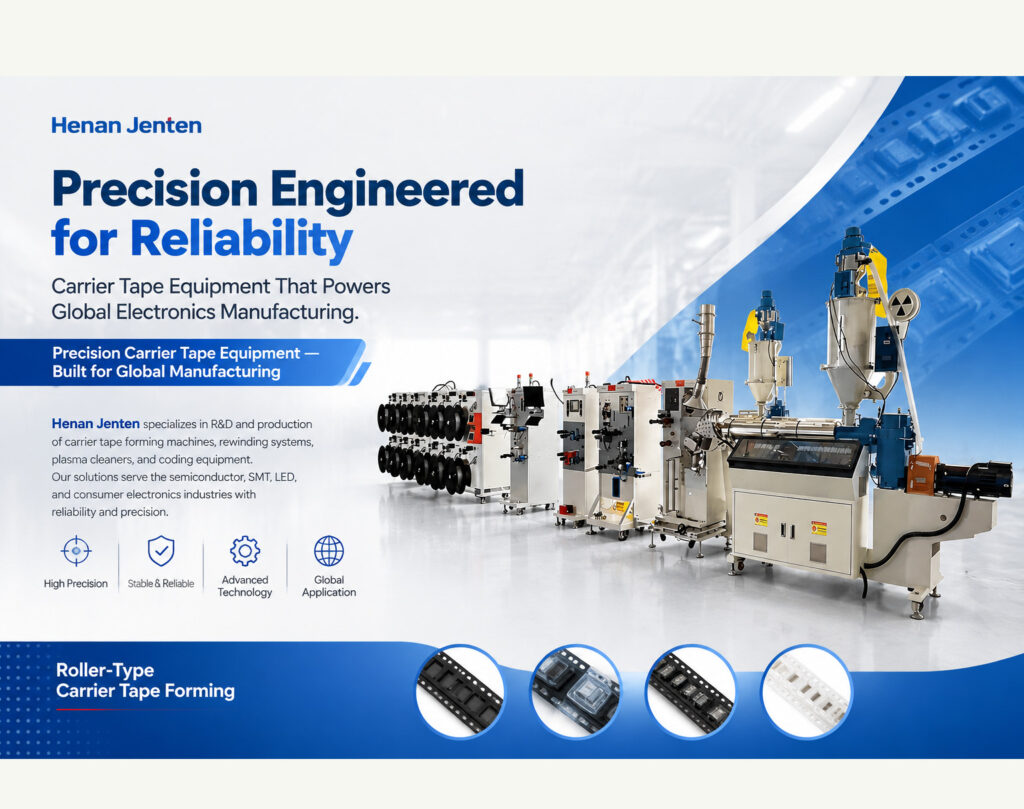
Zhengzhou Jinyingteng (Henan Jenten) manufactures carrier tape forming equipment with independent temperature control for PC, PS, and other thermoplastic materials. This guide covers the technical fundamentals of temperature optimization for both material families.
The Thermal Foundation: Glass Transition Temperature
The glass transition temperature (Tg) establishes the lower boundary for forming. Below Tg, the polymer behaves as a rigid glass. Above Tg, molecular mobility increases, the material softens, and deformation becomes possible.
Polycarbonate has a Tg of approximately 145–150°C . Polystyrene has a Tg of approximately 100°C . This 50°C difference fundamentally shapes the processing windows for each material.
For thermoforming, the sheet must be heated above Tg but below the temperature at which excessive flow or degradation occurs. The processing window—the temperature range between the minimum required for forming and the maximum before material degradation—determines the flexibility available to operators.
Processing Windows for PC and PS
Polycarbonate
PC is an amorphous thermoplastic with a relatively broad processing window. Forming temperatures for PC are typically reported in the range of 130°C to 158°C above the material’s Vicat softening temperature (VST B50), which translates to practical forming temperatures well above 150°C for carrier tape applications .
The material’s high melt viscosity provides a degree of process tolerance. PC resists rapid thinning during forming, which supports more uniform wall thickness distribution across the pocket profile. This characteristic is one reason PC dominates high-precision semiconductor carrier tape applications, where pocket tolerances of 30 micrometers are required .
Polystyrene
PS has a broader processing window in absolute terms but a lower thermal ceiling. Research on amorphous polymers indicates that polystyrene can be thermoformed at temperatures between 127°C and 180°C, giving a processing window exceeding 50°C .
The wider window translates to more forgiving operation. However, PS exhibits higher camber tendencies than PC, which can affect tape tracking if forming and cooling are not carefully controlled . The lower forming temperature also means PS reaches its processing range more quickly, reducing pre-heating requirements.
| 매개변수 | 폴리카보네이트(PC) | 폴리스티렌 (PS) |
|---|---|---|
| Glass transition temperature | ~145–150°C | ~100°C |
| Practical forming window | ~130–180°C | ~127–180°C |
| Melt viscosity | High | 보통 |
| Camber tendency | Low | Higher |
| Typical semiconductor application | WLCSP, BGA, precision ICs | 표준 집적회로(IC), 개별 소자 |
The Critical Role of Pre-Drying
Temperature optimization cannot be separated from moisture control. Both PC and PS are hygroscopic—they absorb moisture from ambient air.
For polycarbonate, the concern is particularly acute. A PC sheet can reach a saturation concentration of 0.3% moisture within 24 hours of exposure to humid air . When heated rapidly during forming, this absorbed moisture converts to steam. The vapor pressure created can produce voids, bubbles, or swirl marks within the softened polymer—defects that may not become apparent until after forming .
Pre-drying before thermoforming is essential. Recommended drying conditions for polycarbonate sheet include temperatures below 250°F (121°C) with drying times ranging from 4 hours for 0.093-inch sheet to 24 hours for 0.236-inch sheet . Dehumidifying ovens are preferred over convection ovens because they remove moisture from the circulating air rather than simply heating it .
For carrier tape production, the enclosed material feed section on Jinyingteng’s forming equipment helps maintain a controlled environment between drying and forming, reducing the moisture re-absorption that occurs when dried sheet is exposed to ambient air.
Temperature Uniformity Across the Sheet
Pocket formation requires that the sheet reaches forming temperature uniformly across the area to be deformed. Temperature gradients produce uneven material flow, leading to pocket depth variation and wall thickness inconsistency.
Radiant heating is the preferred method for carrier tape forming. Infrared or quartz heaters provide contactless, rapid heating that can be precisely controlled. The heating zone typically consists of multiple independently controlled heater elements arranged to provide uniform coverage across the sheet width .
The distance between the heating elements and the sheet surface influences heating rate and uniformity. Typically, a gap of approximately 50 mm to 100 mm is maintained between opposing heater surfaces . This spacing allows radiant heat from adjacent elements to overlap, minimizing edge effects and producing a uniform temperature distribution.
The Forming Window and Material Behavior
Within the processing window, temperature selection involves trade-offs.
Lower forming temperatures (closer to Tg) produce higher melt viscosity. The material resists flow, which can preserve wall thickness but may prevent complete mold conformity for deep or complex pockets. Material may exhibit spring-back after forming if the temperature is insufficient for plastic flow .
Higher forming temperatures reduce melt viscosity, allowing more rapid material flow into the cavity. This improves mold conformity and reduces forming time. However, excessive temperature can cause sagging before vacuum is applied, localized thinning at high-stretch regions, and potential thermal degradation if the upper limit is approached.
For carrier tape, the objective is to achieve complete pocket formation with minimal wall thickness variation. This typically means operating in the middle of the processing window—high enough to ensure adequate flow, but not so high that the material becomes uncontrollable.
Temperature Control on the Forming Equipment
Jinyingteng’s carrier tape forming machines incorporate several temperature control features relevant to PC and PS processing.
Independent heating zone control. Multiple heating elements can be individually adjusted to maintain uniform sheet temperature across the tape width. This capability addresses the edge effects that occur when heating a finite-width sheet.
Pre-heating stage. A pre-heating zone before the forming station raises the sheet temperature gradually, reducing thermal shock and promoting uniform material softening. For PC, which requires higher forming temperatures, controlled pre-heating reduces the temperature differential the material must withstand in the forming zone.
Mold temperature regulation. Water circulation through the mold maintains stable thermal conditions during continuous production. Without active cooling, mold temperature rises as heat transfers from successive heated sheet sections, producing dimensional drift in pocket geometry. The mold temperature also influences the rate at which the formed pocket cools and sets its final dimensions.
Real-time temperature monitoring. Thermocouples or infrared sensors positioned at critical points in the heating and forming zones provide feedback for process control. Operators can verify that the sheet has reached the target forming temperature before vacuum is applied.
Practical Optimization Approach
For a given carrier tape specification—material, pocket dimensions, and production speed—temperature optimization follows a systematic sequence:
- Establish the baseline. Select a starting temperature within the material’s processing window. For PC, this may be 160–170°C; for PS, 140–150°C.
- Evaluate pocket formation. Inspect pockets for completeness, dimensional accuracy, and wall thickness uniformity. Incomplete corners indicate insufficient temperature. Excessive thinning indicates temperature that is too high.
- Evaluate camber and flatness. After forming and cooling, measure the tape’s longitudinal flatness. Excessive camber suggests asymmetric cooling or temperature gradients across the sheet width.
- Iterate within the window. Adjust temperature in small increments (5–10°C) and re-evaluate. The optimal temperature is the lowest value that produces complete, dimensionally stable pockets. Operating at the lower end of the window reduces camber risk and energy consumption.
- Verify at production speed. Temperature requirements may shift as production speed increases. Faster line speeds reduce the dwell time in the heating zone, potentially requiring higher heater output to maintain sheet temperature. Verify that the optimized temperature remains valid at the target production rate.
결론
Forming temperature for PC and PS carrier tape is a controllable process variable, not a fixed equipment setting. The 50°C difference in glass transition temperature between these materials translates to distinct processing windows, different pre-drying requirements, and different tolerance for thermal variation.
Zhengzhou Jinyingteng (Henan Jenten) manufactures carrier tape forming equipment with the temperature control capability needed for both material families. Independent heating zone adjustment, active mold temperature regulation, and real-time monitoring support the process optimization that precision carrier tape production demands.
 KO
 EN_GB
 ID
 VI
 RU